Made and checked in-house
Eight departments on one floor in Aligarh, from the furnace to the packed carton. Your order stays in our hands the whole way.
- 8 departments
- 5 inspection stages
- AQL 2.5 / 4.0
Departments
Sand casting
Brass and iron poured into sand moulds, cast to your design.
Die casting
Molten metal forced into hardened steel dies for repeatable parts.
Power pressing
A line of presses cuts, forms and punches brass, iron and steel.
Tool room
Lathe, surface grinder, vertical milling and drilling for our own dies.
Polishing and buffing
Casting marks removed, then a bright surface ready for plating.
Plating
Nickel, chrome, gold, antique, black nickel and more, in-house.
Electrophoretic lacquer
An even polyurethane-acrylic coat that seals the finish.
Quality control
Five inspection stages and AQL sampling before dispatch.
Cast, pressed, polished and plated
Brass and iron are poured into sand moulds for knockers, knobs, hinges and decorative pieces. Die casting forces molten metal into hardened steel dies for large runs, and a line of power presses cuts, forms and punches sheet metal.
Our tool room makes and maintains the dies and fixtures, so a new design goes from drawing to first samples without waiting on outside toolmakers. Polishing removes casting marks; buffing brings up the bright surface plating needs. Electrophoretic lacquer then seals the finish evenly, in place of spraying and solvents.
Plating done in-house
Nickel · Nickel chrome · Chrome · Satin nickel · Satin chrome · Gold · Satin and shine gold · Antique · Black antique · Silver antique · Brushed nickel · Brushed chrome · Black nickel · Gloss and matt colours · Your own finish
What leaves the line
View all designs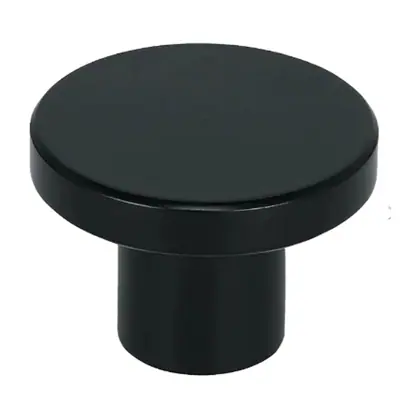 Black Antique Cabinet KnobOCE-CB-101
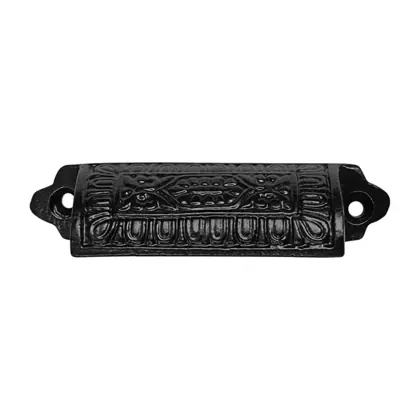 Black Antique Drawer PullOCE-CB-201
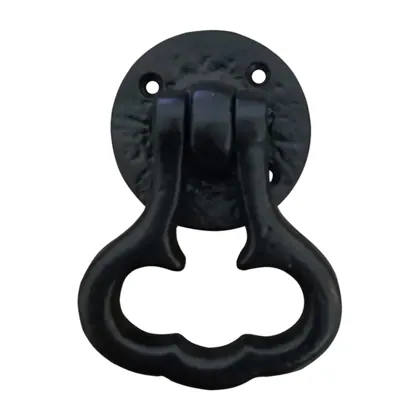 Black Antique Ring Drop PullOCE-CB-301
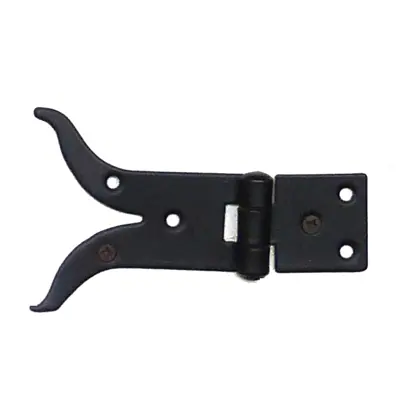 Black Antique Cabinet HingeOCE-CB-401
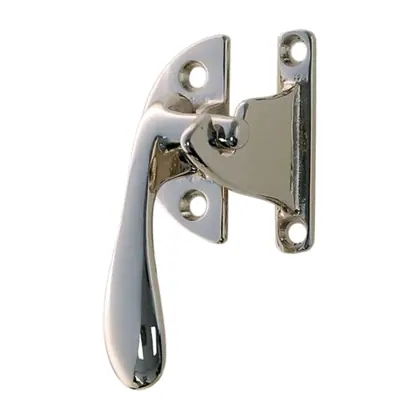 Polished Chrome Cupboard LatchOCE-CB-501
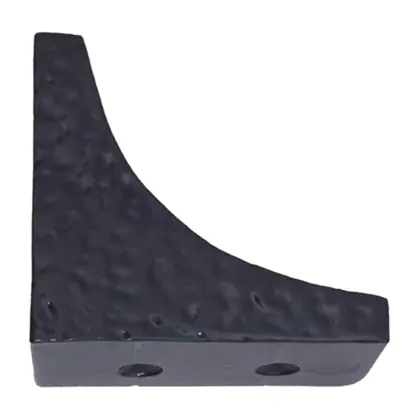 Black Antique Corner BracketOCE-CB-601
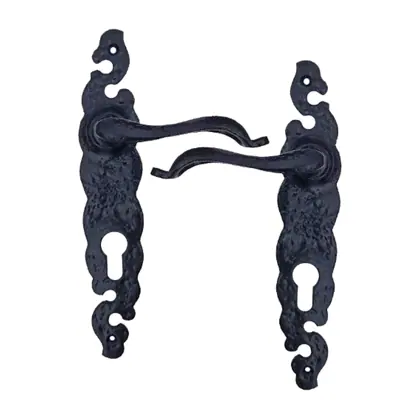 Ornate Scroll Lever HandleOCE-DH-101
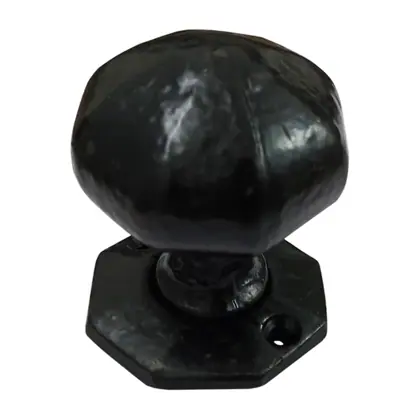 Black Antique Mortice Door KnobOCE-DH-201
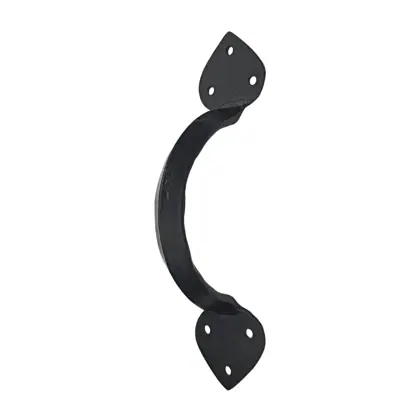 Black Antique Door & Cabinet Pull 8″OCE-DH-301
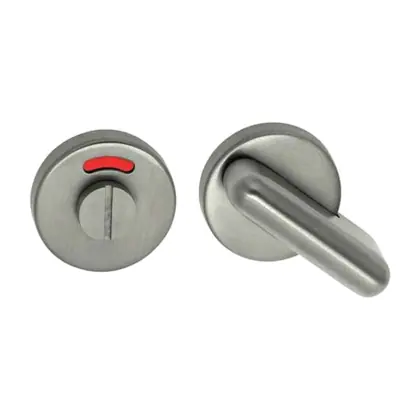 Polished Chrome Turn & ReleaseOCE-DH-401
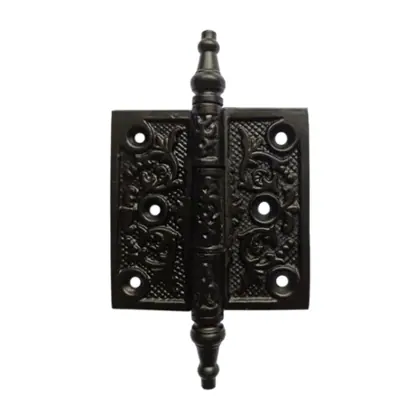 Black Antique Decorative HingeOCE-DH-501
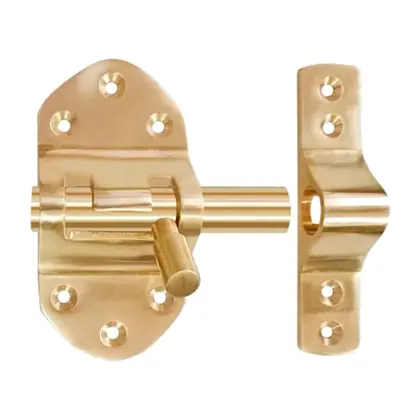 Polished Brass Barrel BoltOCE-DH-601
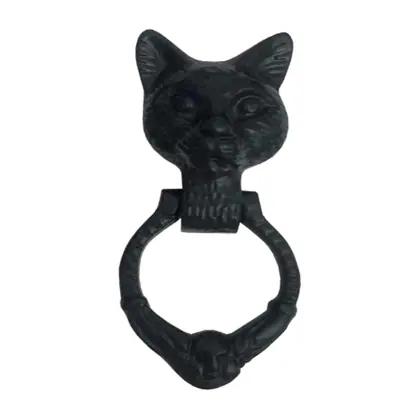 Black Antique Door KnockerOCE-DH-7001
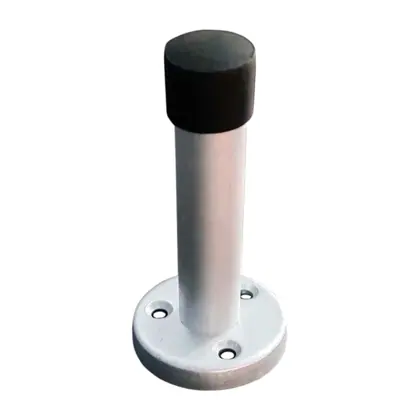 Satin Anodised Door StopOCE-DH-801
The approved sample is the standard
We make builders hardware that matches what you approved, in finish, size and function, on every order. We build quality in at each stage, measure it before every shipment, and keep improving the way we work.
- Incoming materialBrass, iron, steel and castings checked for grade and defects.
- After casting and pressingDimensions checked; blow holes, cracks and burrs rejected.
- After machiningThreads, hole positions and fit with screws checked.
- After platingColour against the approved sample, coverage and adhesion.
- Final inspectionFunction, count and packing checked; AQL sampling per lot.
Every lot is sampled to AQL
ISO 2859-1 (ANSI/ASQ Z1.4), general inspection level II, single sampling. If defects reach the reject number, the lot is sorted or reworked and inspected again before it ships.
Critical (0): unsafe or unusable, such as a cracked casting or a lock that does not work. Major (2.5): fails in use or sale, such as peeling plating or a size out of tolerance. Minor (4.0): cosmetic only.
| Lot size (pcs) | Code | Sample | Critical | Major | Minor |
|---|---|---|---|---|---|
| 91 – 150 | F | 20 | 0 / 1 | 1 / 2 | 2 / 3 |
| 151 – 280 | G | 32 | 0 / 1 | 2 / 3 | 3 / 4 |
| 281 – 500 | H | 50 | 0 / 1 | 3 / 4 | 5 / 6 |
| 501 – 1,200 | J | 80 | 0 / 1 | 5 / 6 | 7 / 8 |
| 1,201 – 3,200 | K | 125 | 0 / 1 | 7 / 8 | 10 / 11 |
| 3,201 – 10,000 | L | 200 | 0 / 1 | 10 / 11 | 14 / 15 |
| 10,001 – 35,000 | M | 315 | 0 / 1 | 14 / 15 | 21 / 22 |
Accept / reject numbers. Larger lots and tighter levels on request.